

Belt Conveyor

Belt Conveyor
Underground Solutions Provider
China Railway Engineering Equipment Group Co., Ltd. is committed to making tunnel construction better, faster and safer. Within this, the belt conveyor, as a key link in tunnelling operation, has always been the core focus of technological innovation and research and development, creating green, low‑carbon, stable and efficient material transportation solutions for global customers.
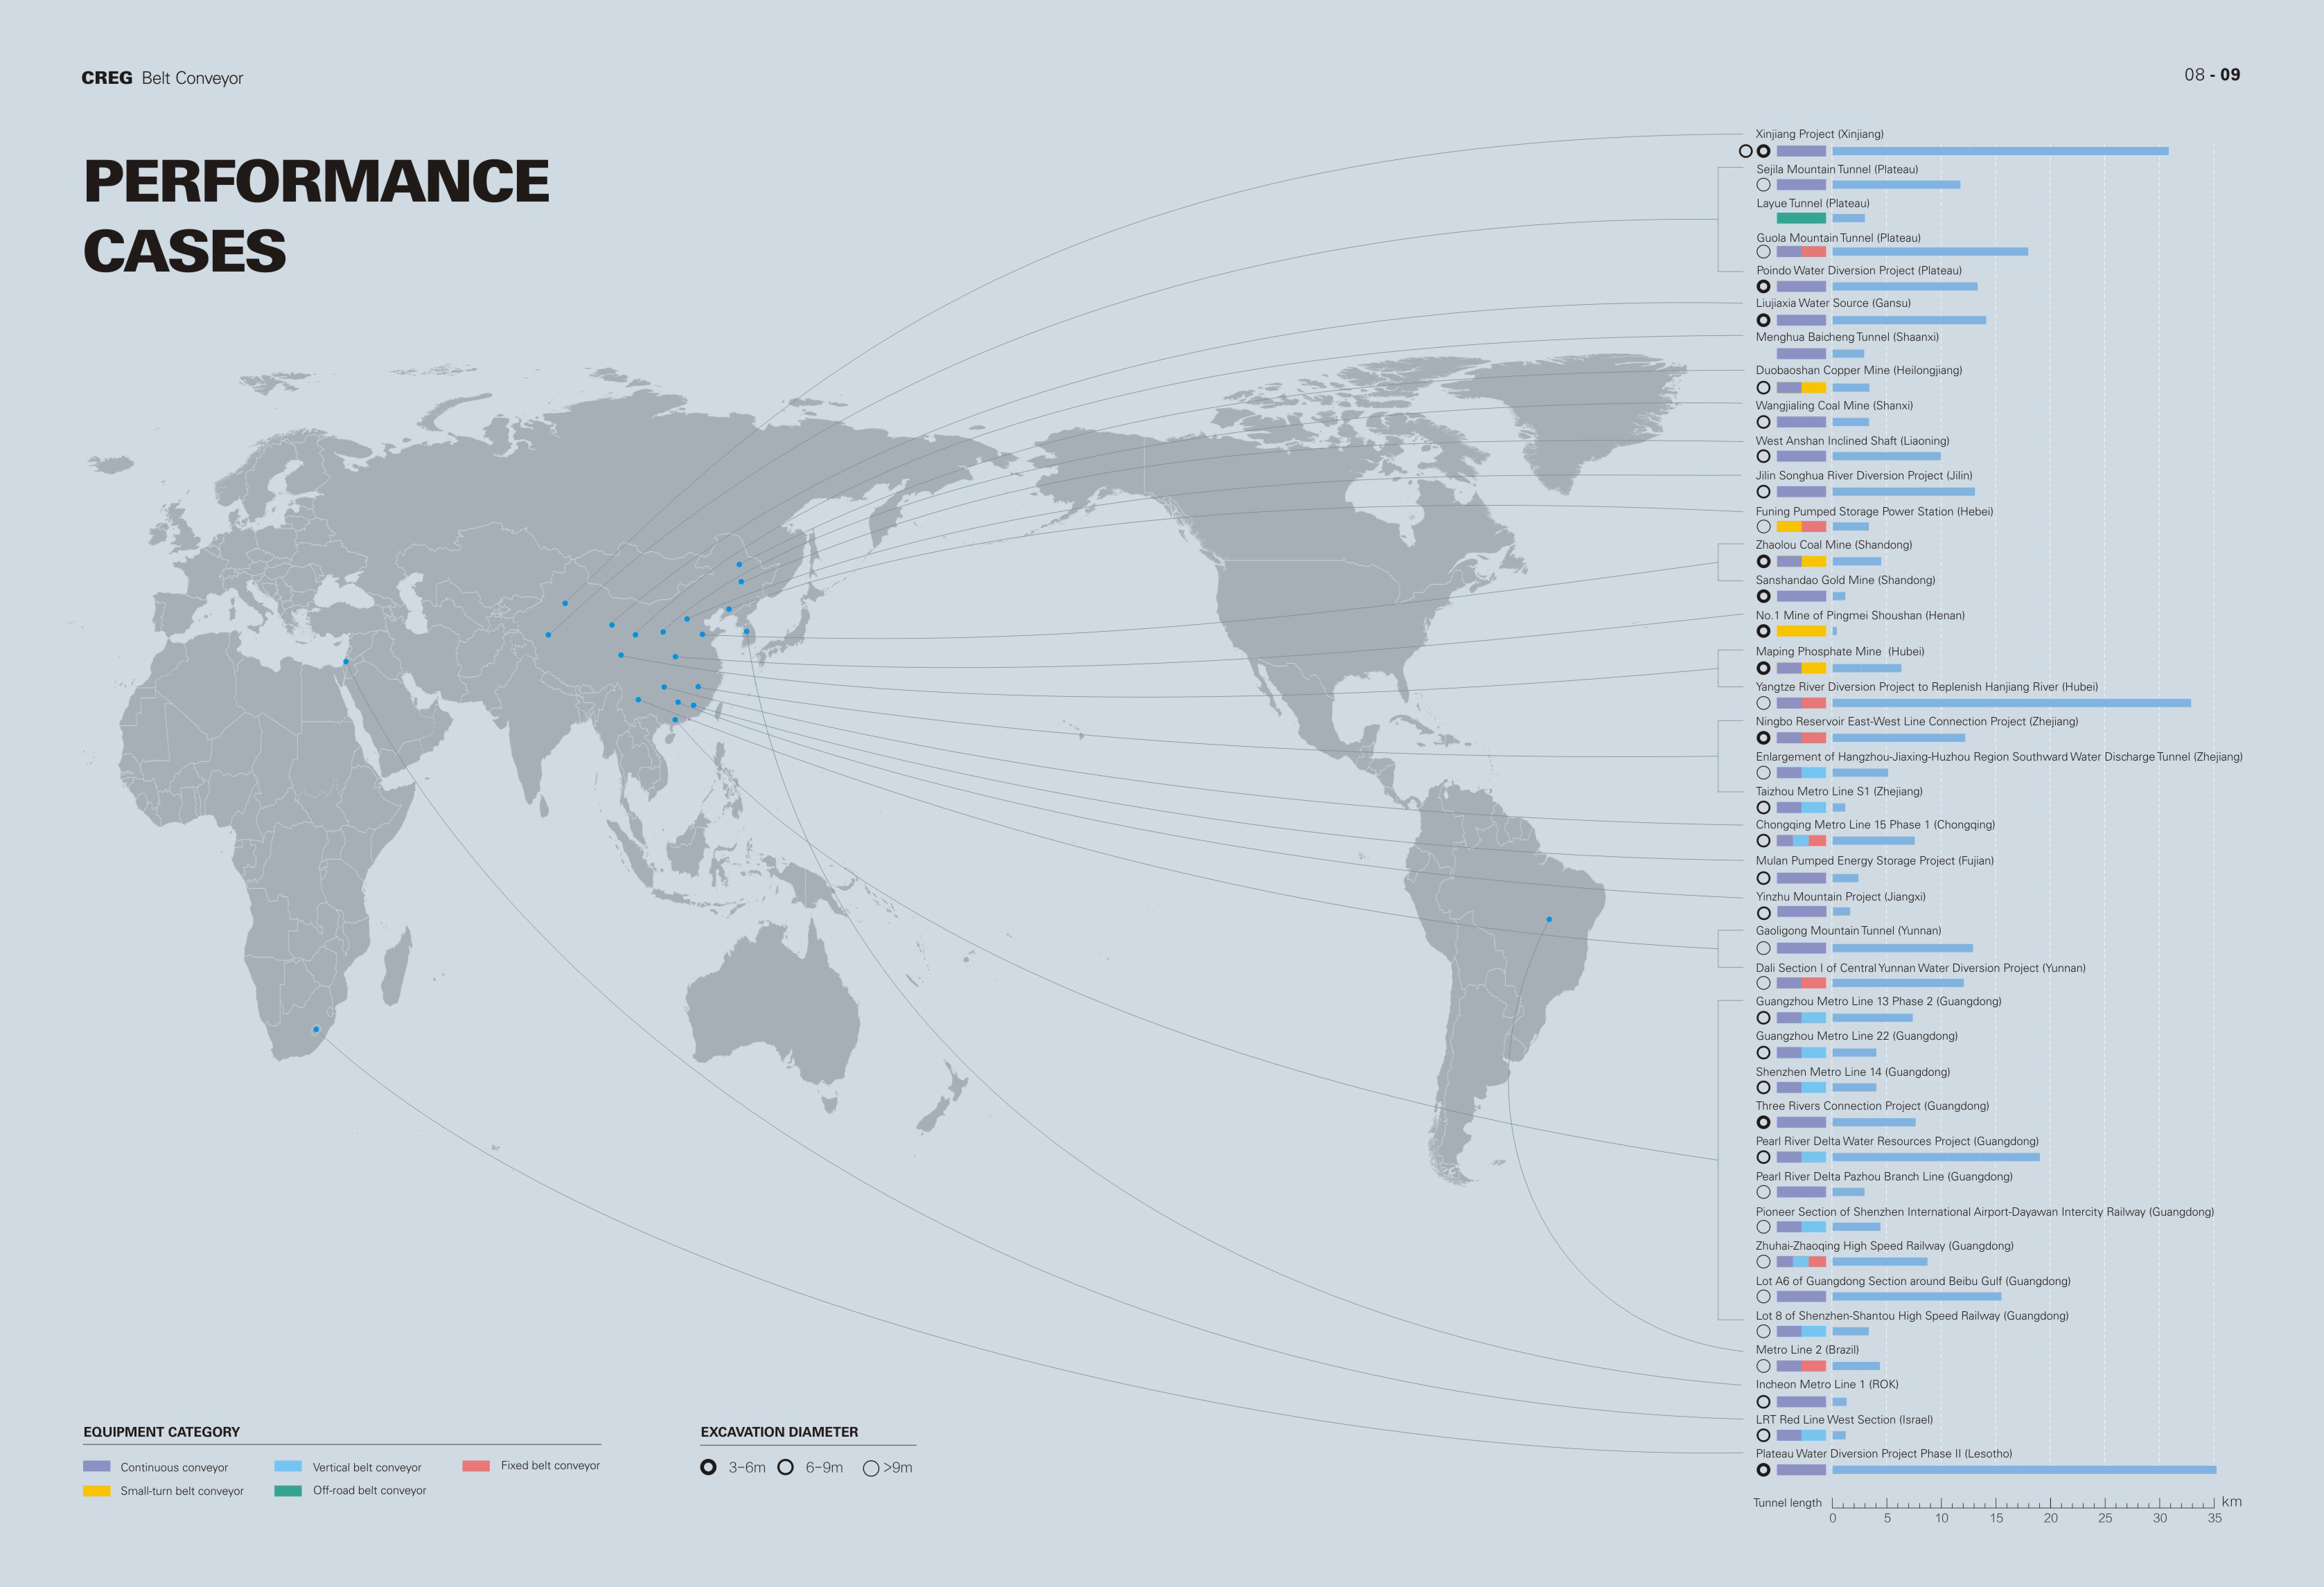
As an integrated service provider of belt conveyors, CREG offers a wide range of solutions in terms of long‑distance continuous conveyors, vertical lifting belt conveyors, small‑turn belt conveyors and off‑road belt conveyors. To date, the company has successfully provided comprehensive solutions for more than 500 projects across sectors such as railways, highways, metros, water conservancy, hydropower, public utilities and mining energy.
CREG not only focuses on maintaining a strong presence in the domestic market, but also actively expands its international business. It has successfully exported advanced products and services to many countries and regions across Europe, Asia, Africa and America, demonstrating its strong and growing global competitiveness and brand influence.
With an excellent technical strength, rich project experience and an efficient service system, CREG collaborates with global customers to address diverse challenges in tunnelling. This ensures safe performance and efficient progress of projects, creates maximum value for customers and helps pave a solid path to the future.
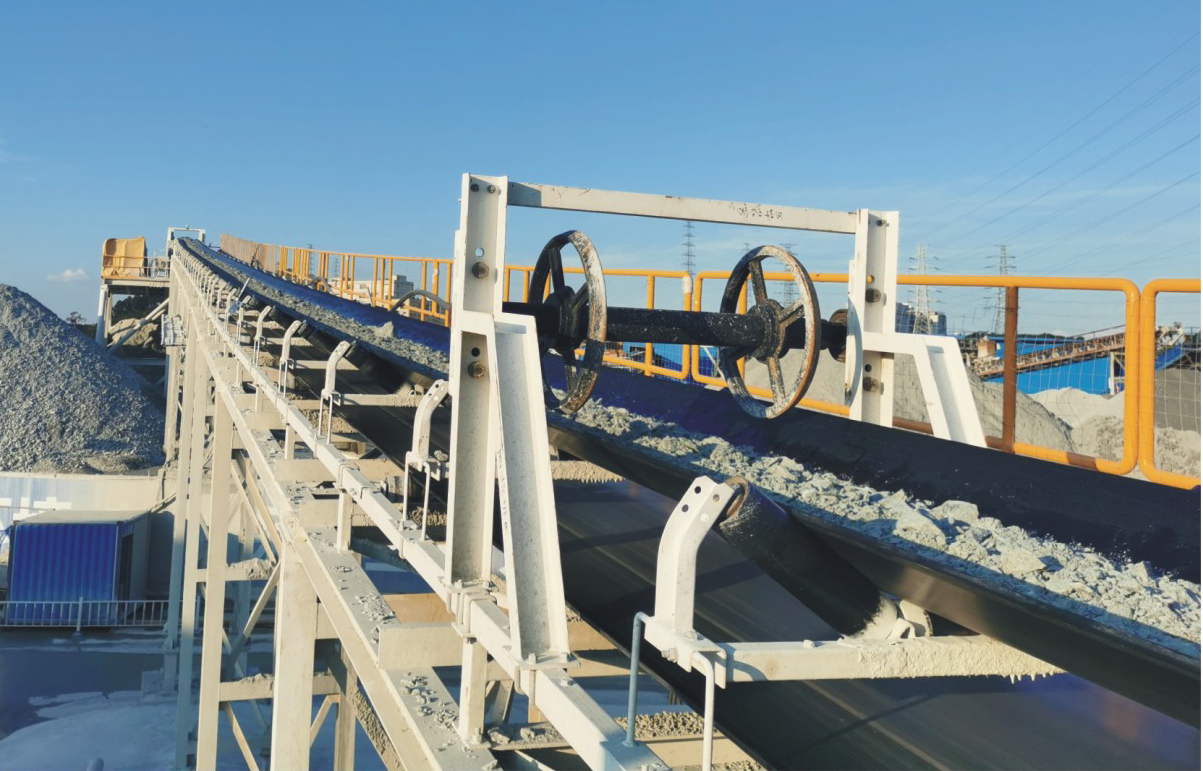
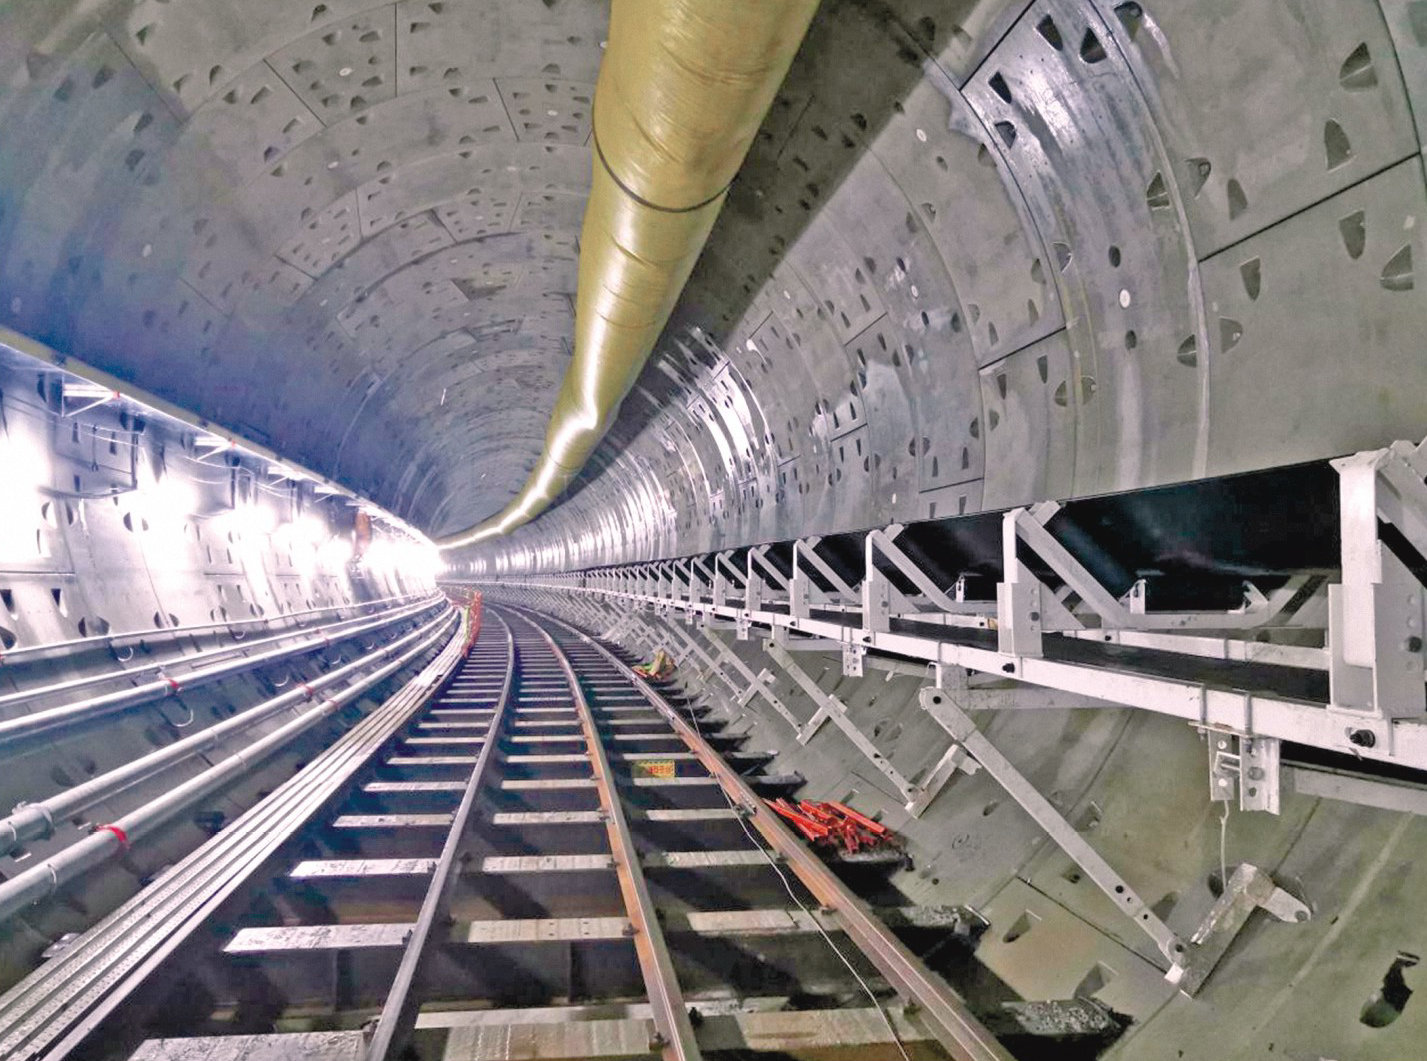
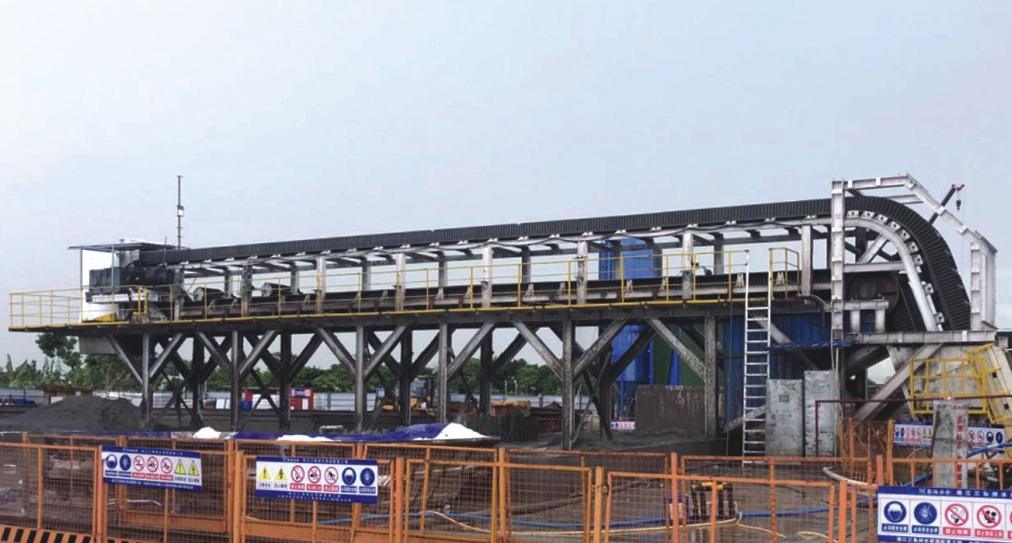
Ultra‑long continuous belt conveyor boosts the construction of the Pearl River Delta Water Resources Allocation Project.
TUNNEL FIELD Solution
Continuous extension belt conveyor
Suitable for shield/TBM continuous tunnelling
Enable extension without shutdown
The belt storage cassette can be installed horizontally or vertically, with a belt storage capacity of 200‑800m
Equipped with an Automatic frequency conversion tensioning system
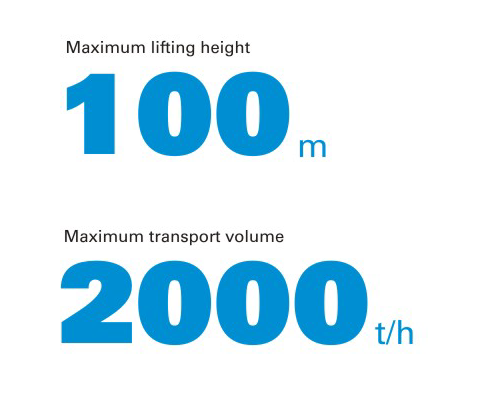
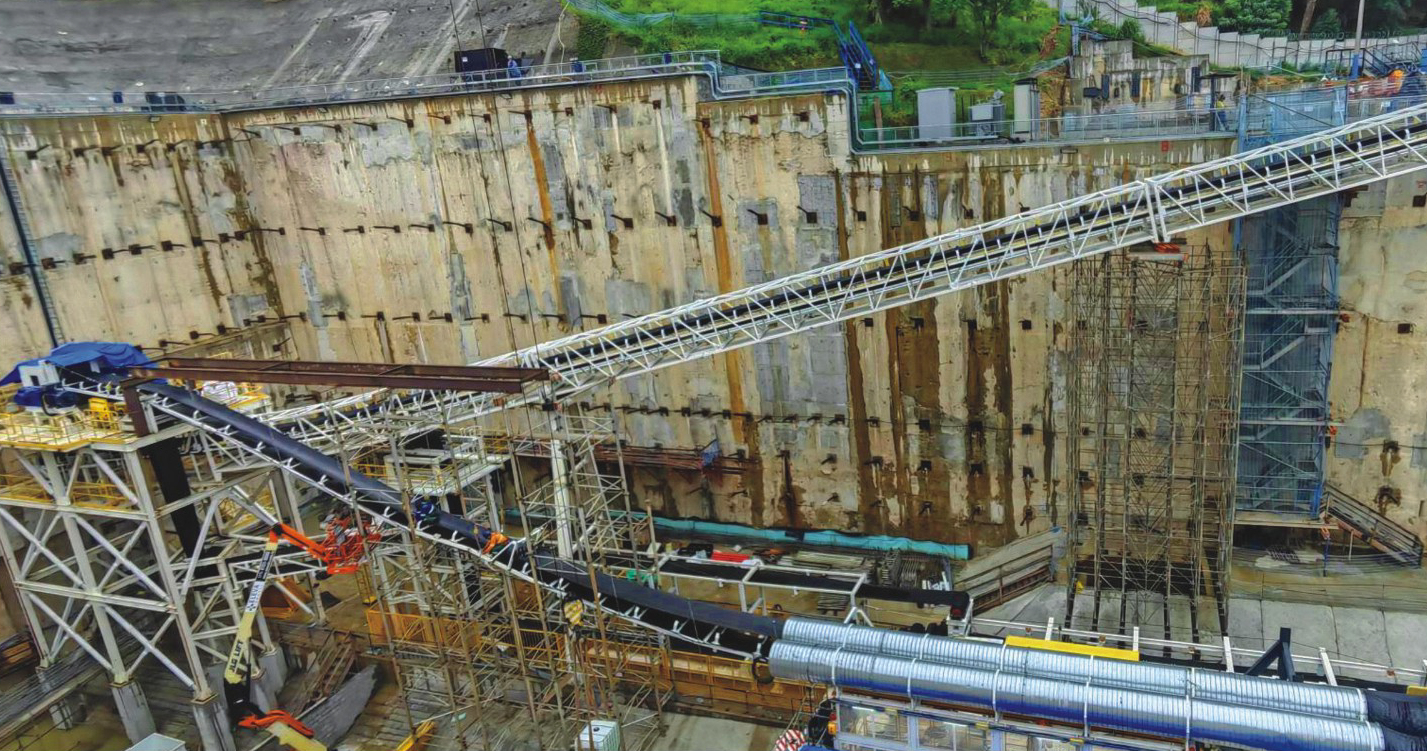
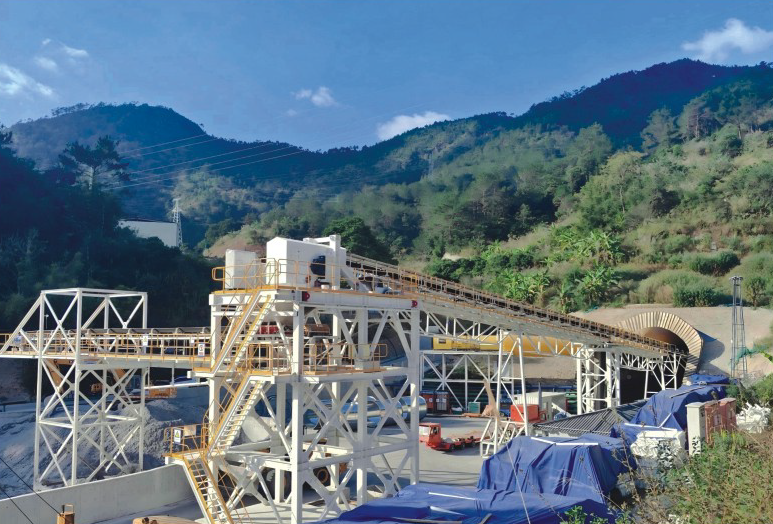
Vertical lifting belt conveyor
Vertical lifting solution for bulk materials
Standard section and modular design, convenient for efficient disassembly and assembly
Embedded with special skeleton material to prolong the service life of rubber belt
Multiple sweeping and cleaning systems to effectively reduce slags in the return stroke
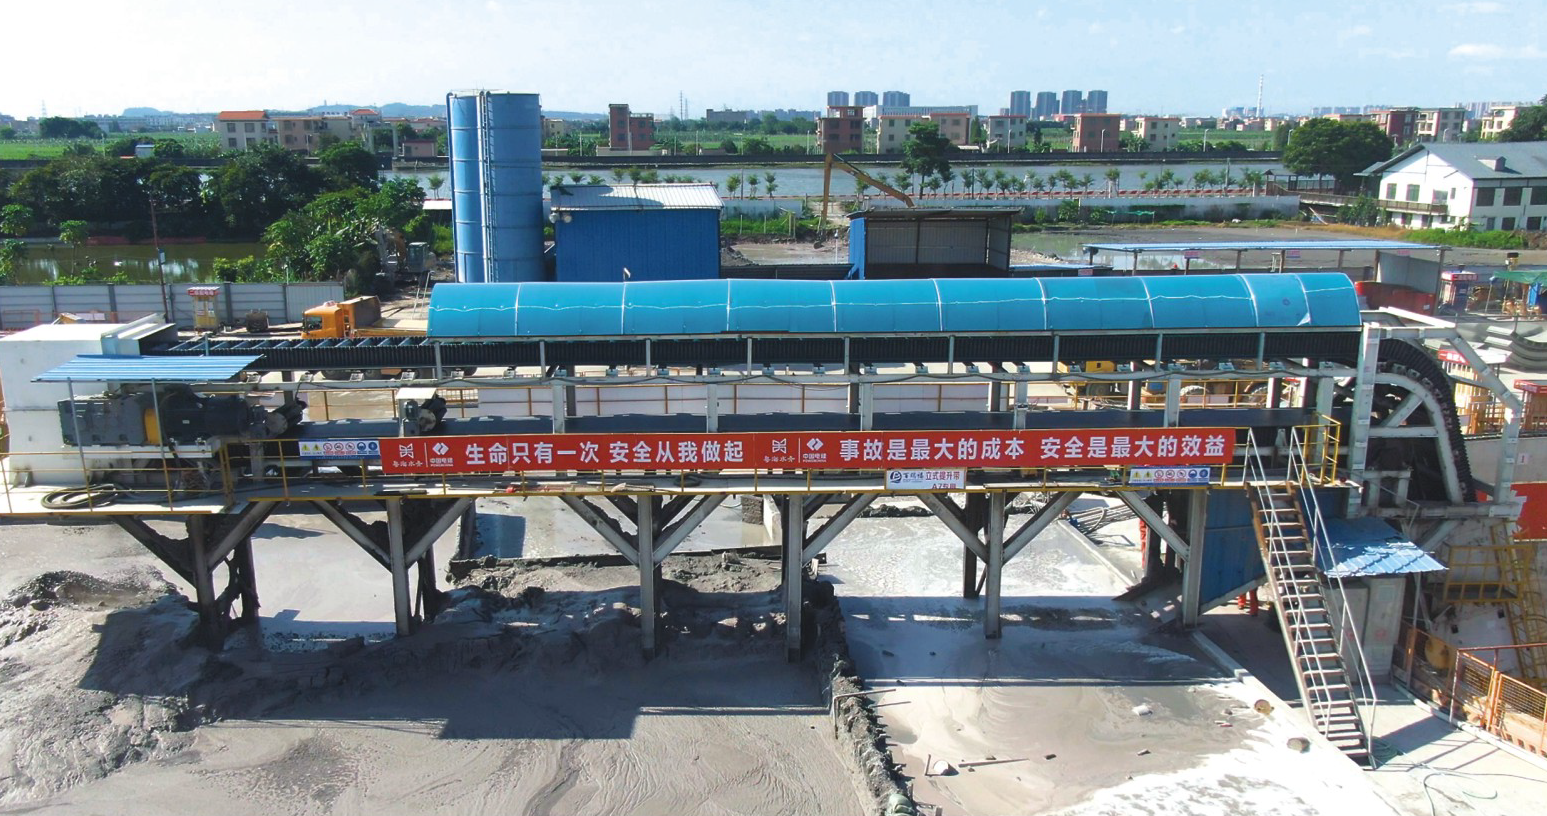
First‑time achievement of continuous vertical transportation in a 75m ultra‑deep shaft.
MINING FIELD Solution
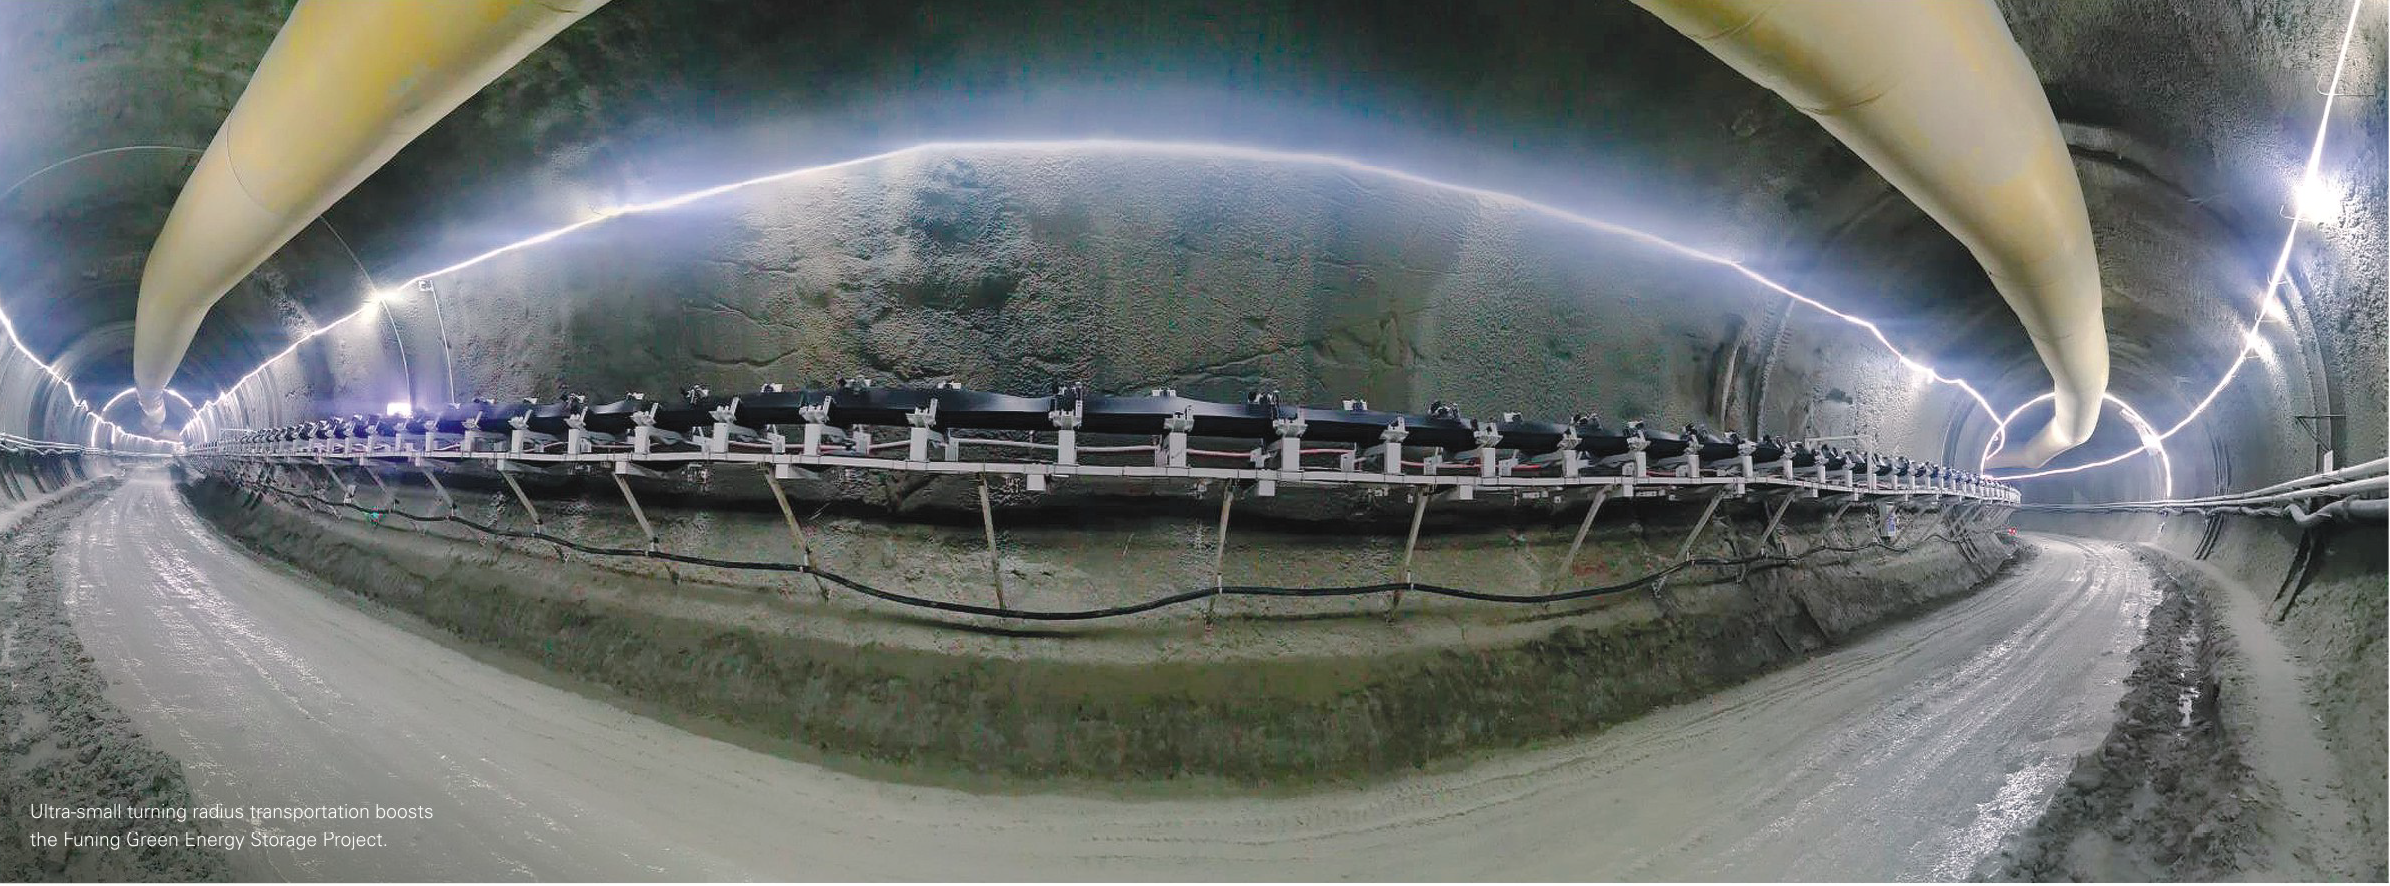
Small‑turn belt conveyor
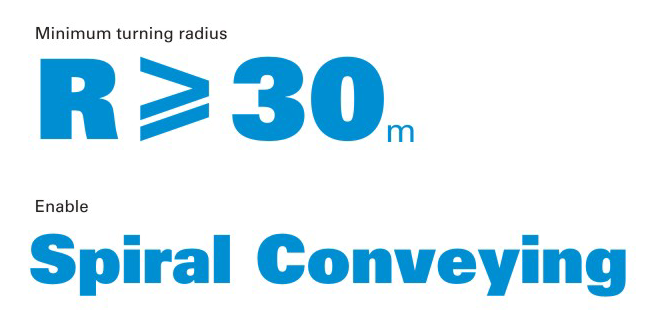
Designed for conveying with turning radius less than R250m
Customized flexible conveyor belt
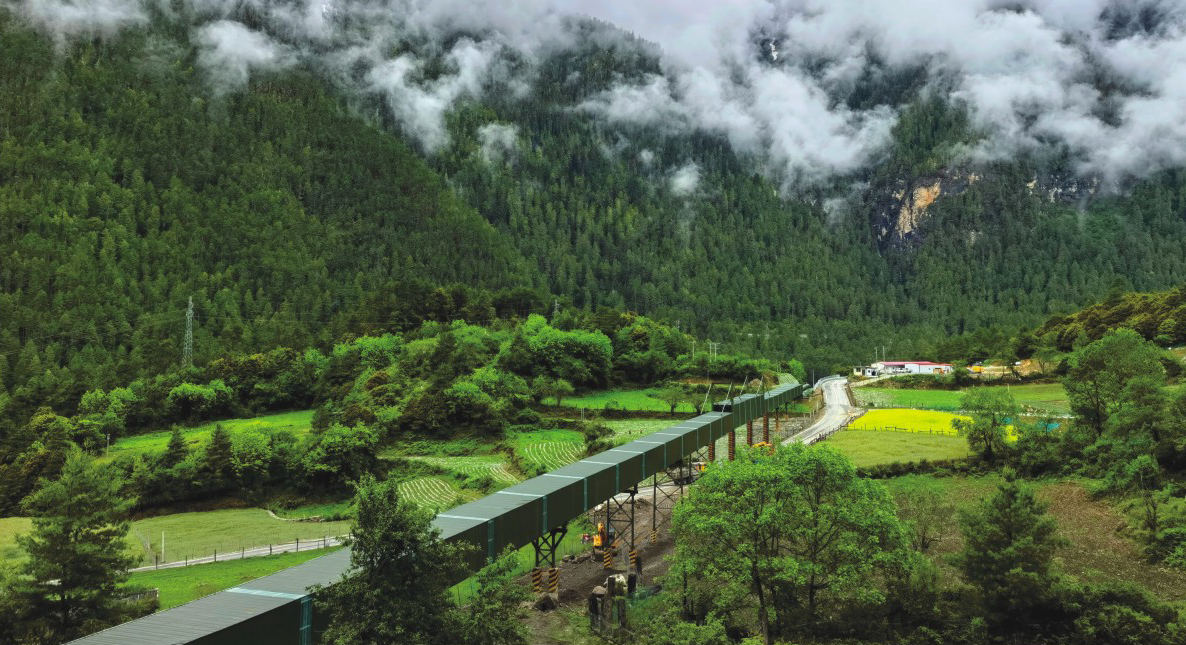
Off‑road belt conveyor
Solution for long‑distance transportation of bulk materials in complex geological formations
Fabricated long‑span design
Optional closed design

The fully enclosed off‑road belt conveyor passes through the nature reserve in a safe and environmentally friendly manner.
Functions and Applications of Special Belt Conveyor Systems for Tunnel Engineering
1. Core Advantages and Adaptation Features
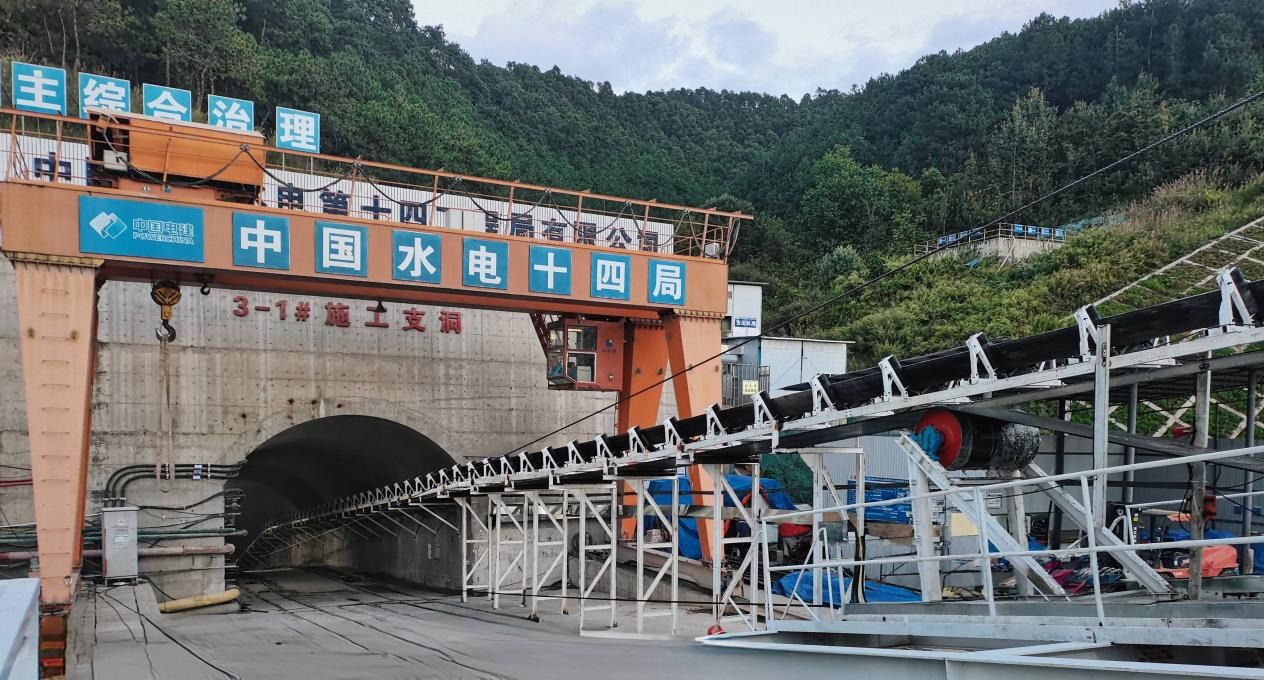
The special belt conveyor system for tunnels can seamlessly connect and cooperate with all types of tunnel boring equipment. It dynamically adjusts the muck removal speed in accordance with the tunneling rate, realizing synchronous operation of tunneling and mucking processes. Adopting a fully automatic working process, the system greatly reduces on-site labor allocation and cuts labor costs. Boasting strong adaptability to complex working conditions, the equipment is applicable to special tunnel construction scenarios including small-radius turns, edge construction, slopes of up to 15° and vertical conveying, outperforming traditional muck removal equipment.


2. Engineering Application Value of Belt Conveyor Systems
Modern mechanized tunneling delivers high construction efficiency. With mature construction technologies, a weekly tunneling progress of hundreds of meters is achievable in most strata. An efficient and stable muck removal system is the cornerstone of construction progress. Serving as a key hub connecting tunnel boring machines and ground construction sites, the belt conveyor system enables continuous and stable removal of tunnel muck and stones. Professional brands customize and develop high-performance belt conveyor systems tailored for the specific working conditions of tunnel construction, which adapt to various geological environments such as soft and hard rock strata and composite strata, providing reliable conveying support for tunneling operations.
3. High Efficiency and Flexibility for Long-Distance Conveying
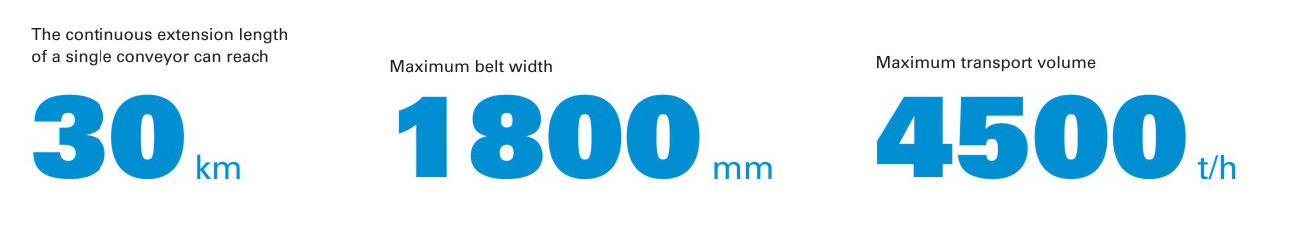
Belt conveying is the most direct, economical and efficient method for tunnel muck removal. Under rapid tunneling conditions for large-section tunnels with a diameter of 8 to 9 meters, the daily earthwork excavation volume can exceed 10,000 cubic meters. As the tunneling depth increases, the maximum single-section muck conveying distance can reach 15 kilometers, making long-distance and large-volume conveying a core construction challenge. Equipped with horizontal and vertical belt storage devices, the system can extend the conveyor belt length in real time according to construction progress and site conditions without frequent equipment disassembly and assembly, greatly improving construction flexibility. For underground low-level openings such as shafts, vertical or upward belt conveyors are applied to transport muck to the ground. The supporting muck stockpiling system can be precisely arranged based on on-site conditions to achieve efficient and organized stacking of earthwork.

4. Intelligent Protection to Ensure Safe Construction
As a highly integrated high-tech system, the belt conveyor system delivers ultra-high conveying capacity and high efficiency, while minimizing on-site manual intervention, effectively reducing construction safety risks and labor costs. It operates stably even under complex working conditions including small-radius turns and large slopes, avoiding muck spillage and equipment stalling. Fitted with front auxiliary drive devices, the system buffers belt tension and reduces equipment wear during turning operations to ensure safe muck conveying. For long-distance straight sections, the auxiliary drive provides supplementary power and reduces energy consumption, effectively improving the overall operational efficiency and stability of the belt conveyor system while balancing construction safety with operational performance.
5. Accurate Synchronization with Tunneling Operation
Efficient tunnel construction relies on the close coordination between tunnel boring hosts and supporting logistics systems. High-quality muck conveying equipment can maximize the working efficiency of tunnel boring machines. Professional technical teams customize dedicated tunnel belt conveyor solutions based on on-site geological conditions, tunneling rates, conveying volumes and site layouts, building a high-precision and high-efficiency muck removal system to ensure smooth and lag-free muck removal operations. The precise synchronization and efficient adaptation between belt conveyor systems and tunneling equipment are crucial for improving the quality and efficiency of tunnel projects and ensuring on-time completion.
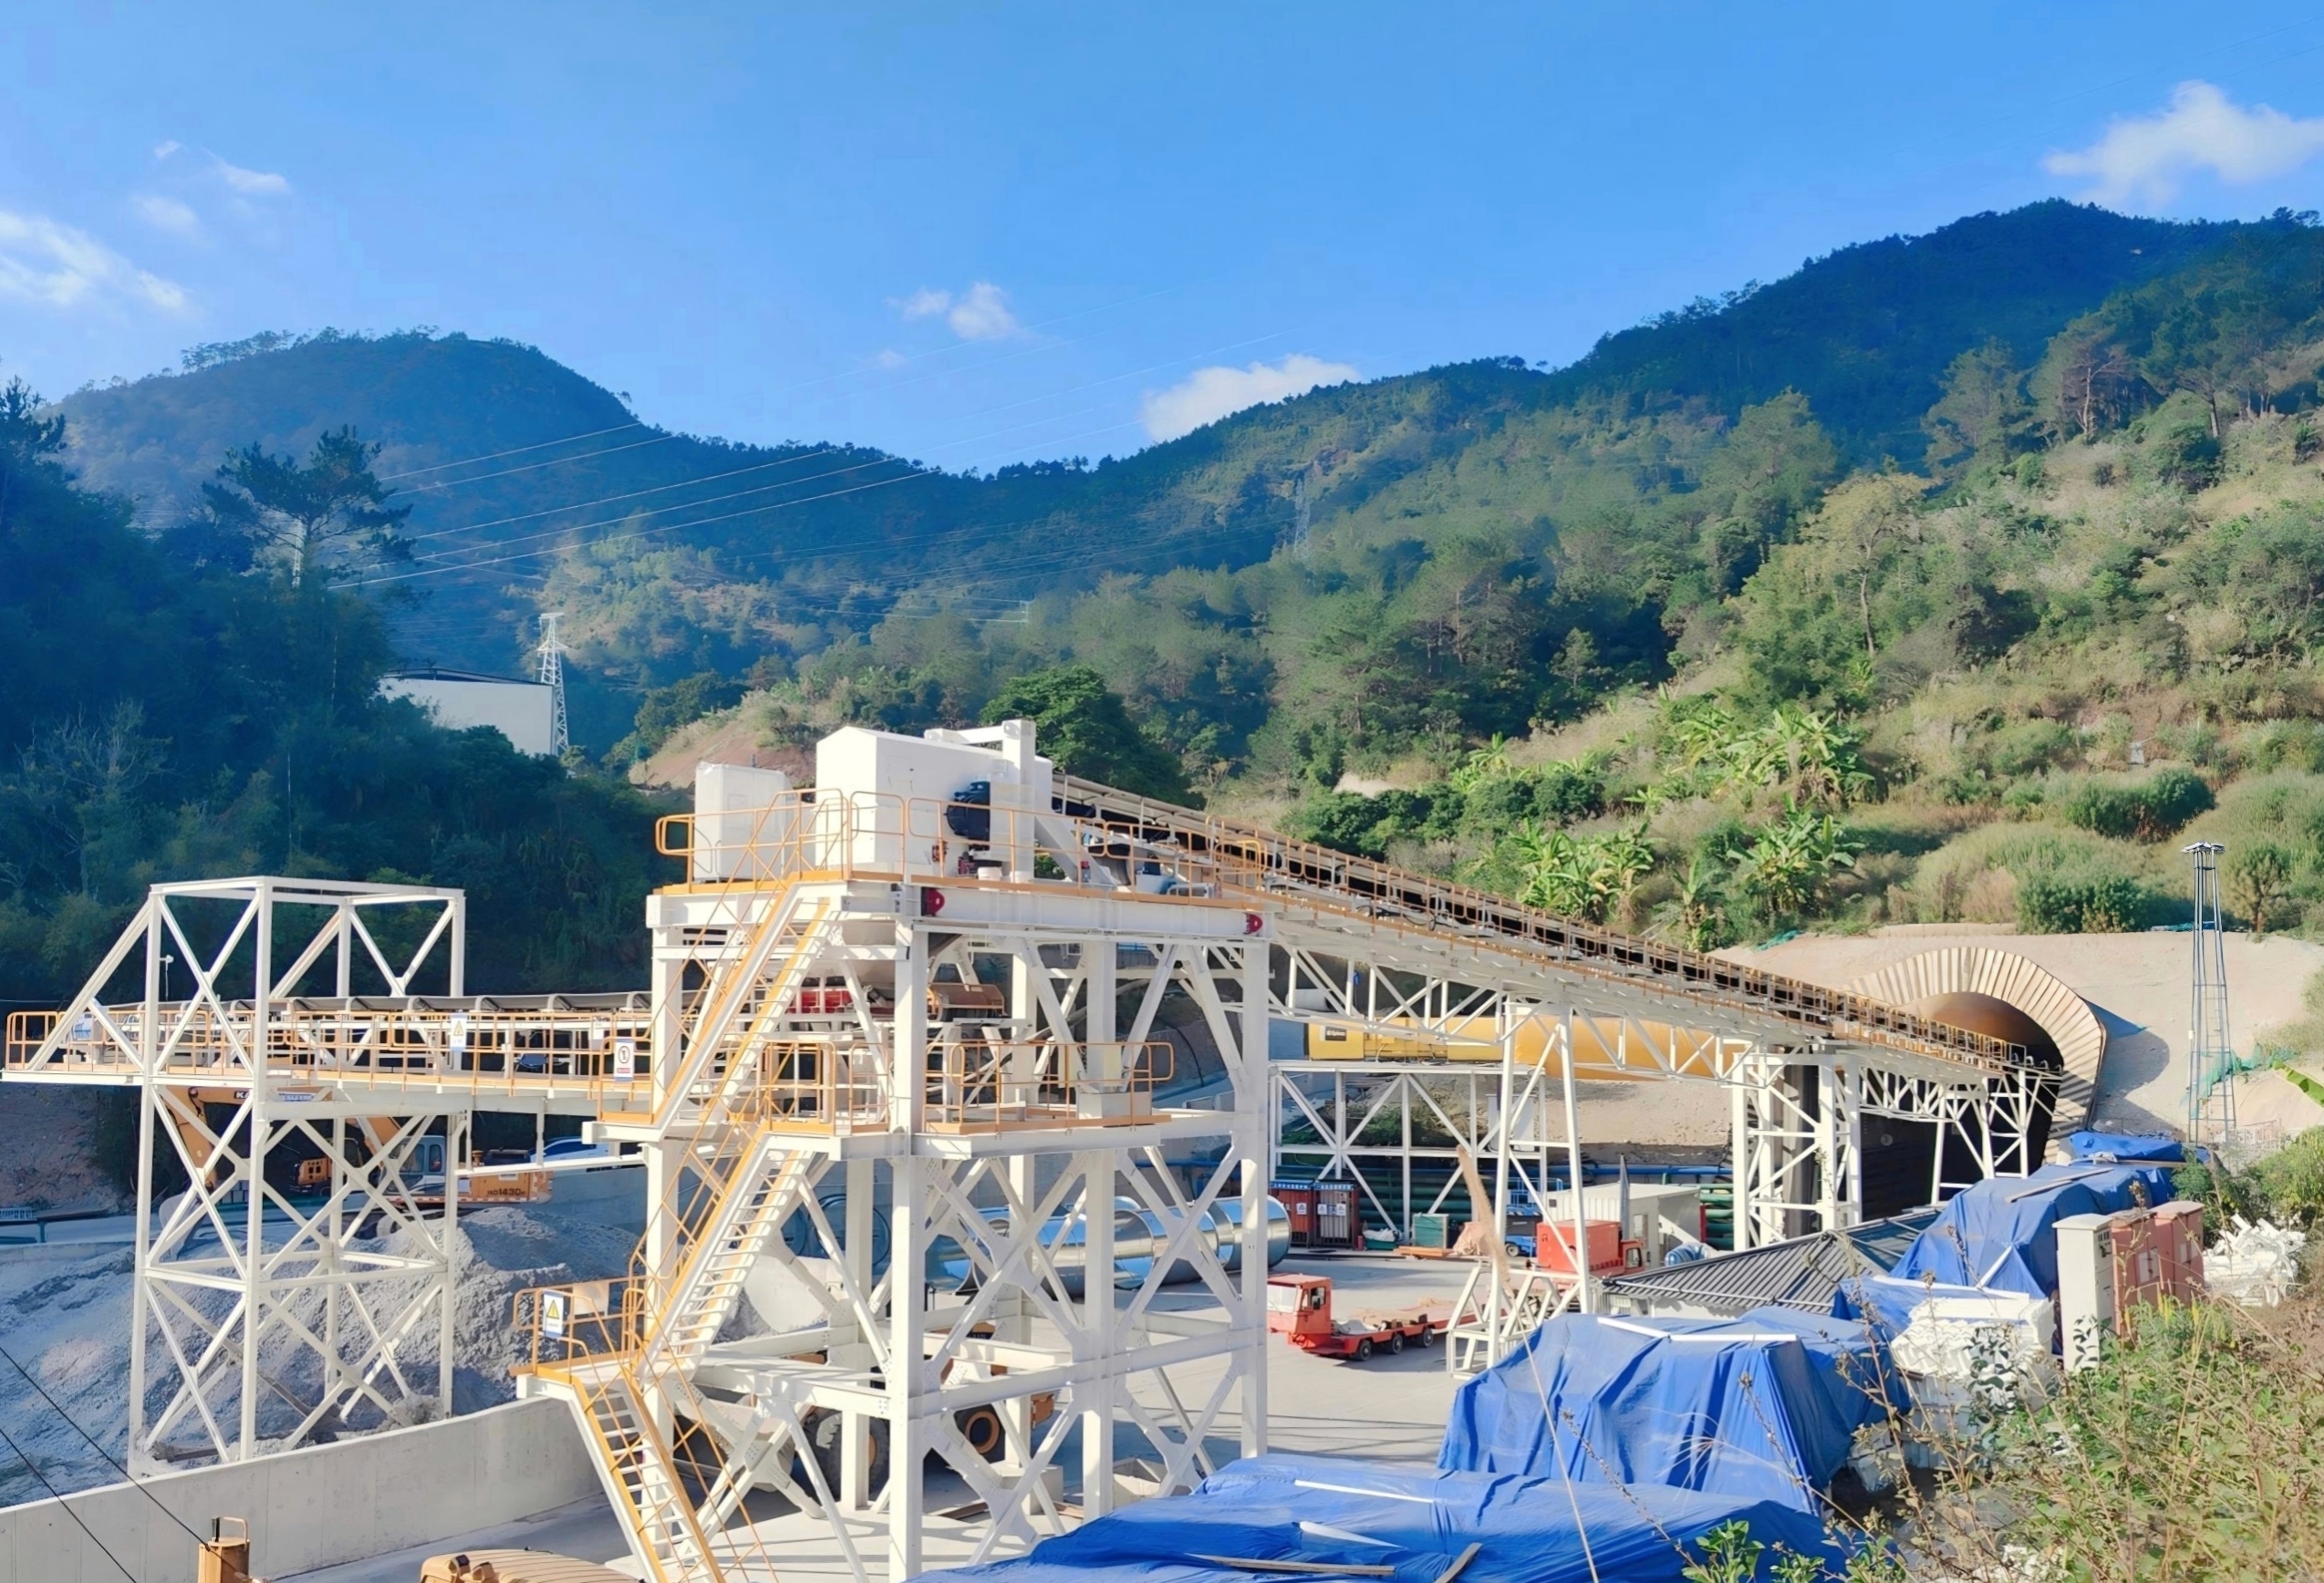
reference project
Full Range Services
CREG also provides high value-added customized services, including design, consultancy, tunnelling service, maintenance, remanufacturing, mechanical & electrical installation, technical service, spare parts, etc. CREG establishes remote support system for delivered TBMs to facilitate CREG rendering quick troubleshooting and real-time monitoring during tunneling.
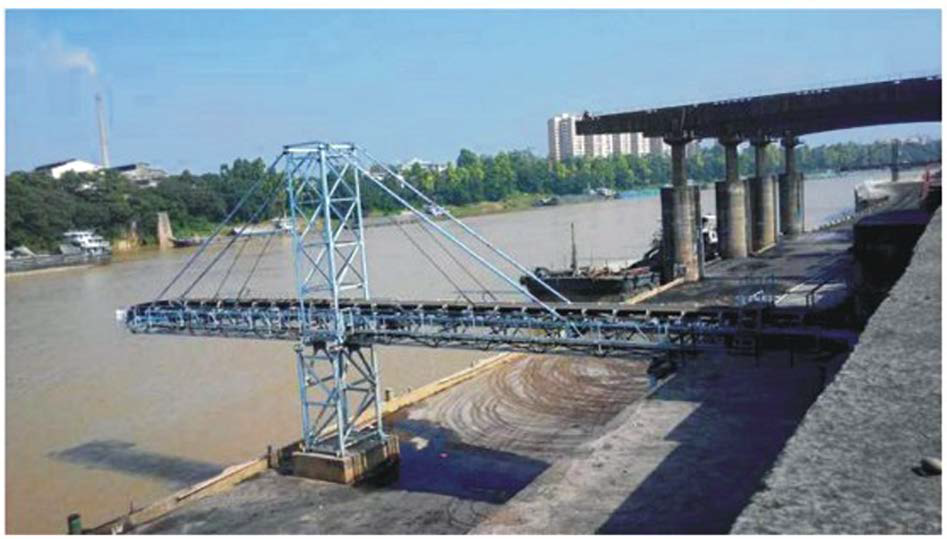
Ship loader
The ship loader is a large‑scale conveying equipment used for bulk material shipment at the wharf. It enables continuous transportation of materials from the stockyard to the cabin quickly completing the loading operation.
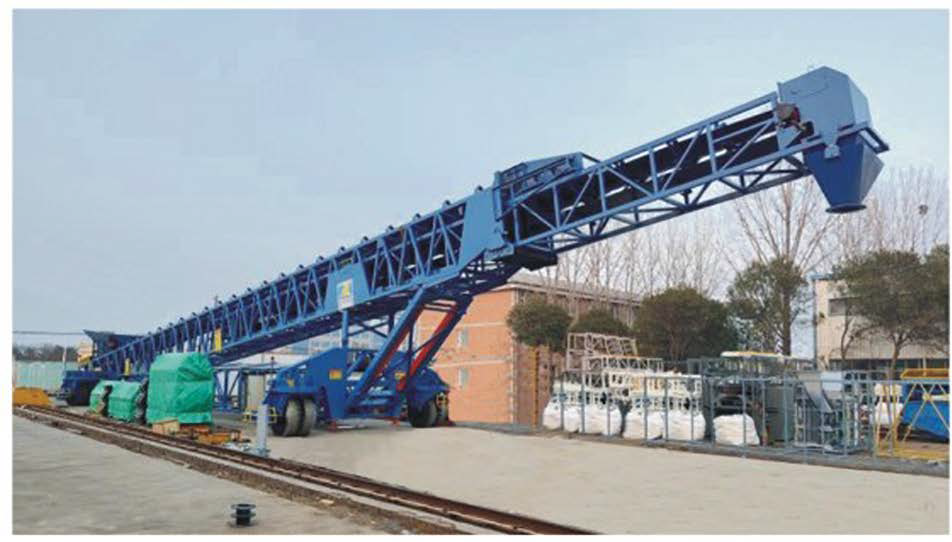
Stacker
The stacker is a large conveying equipment for bulk material stacking, which enables efficient transfer of materials to the storage yard.
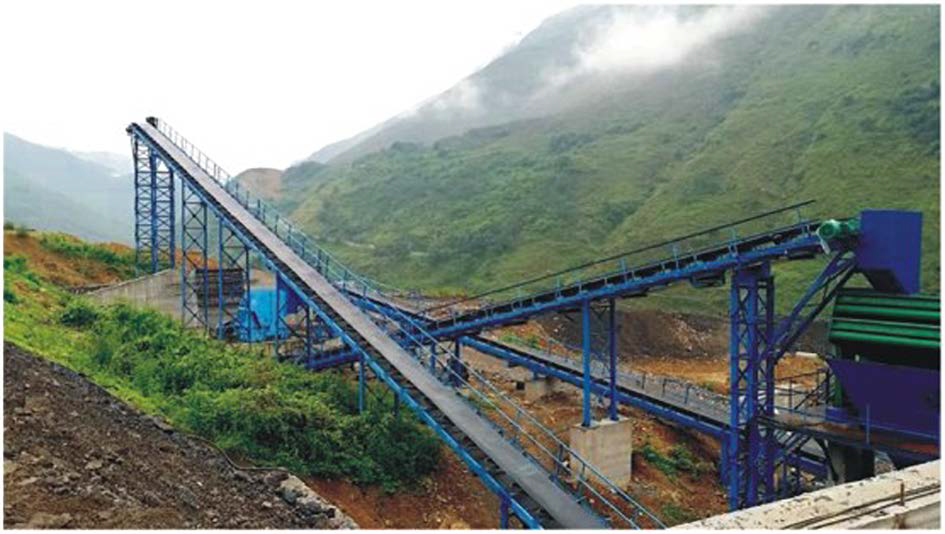
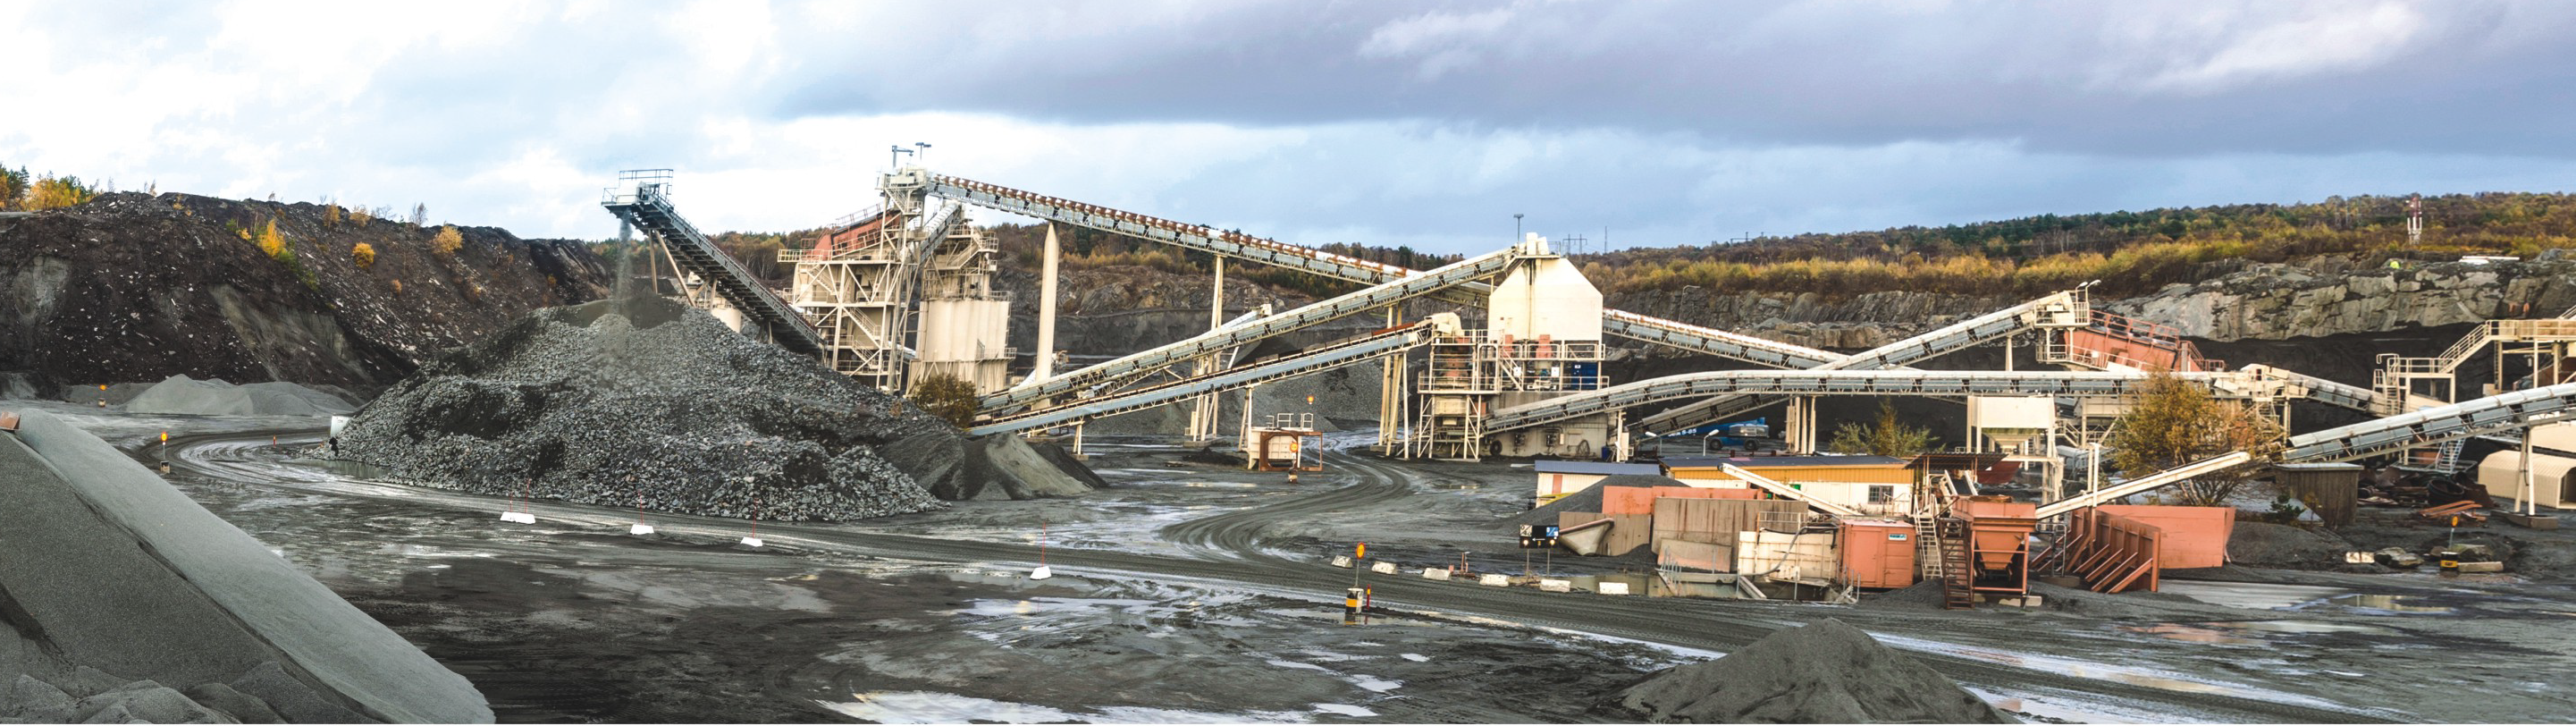
Sandstone aggregate belt conveyor
The sandstone aggregate belt conveyor has efficient and stable transfer capacity, which can meet the material transportation requirements under various working conditions.
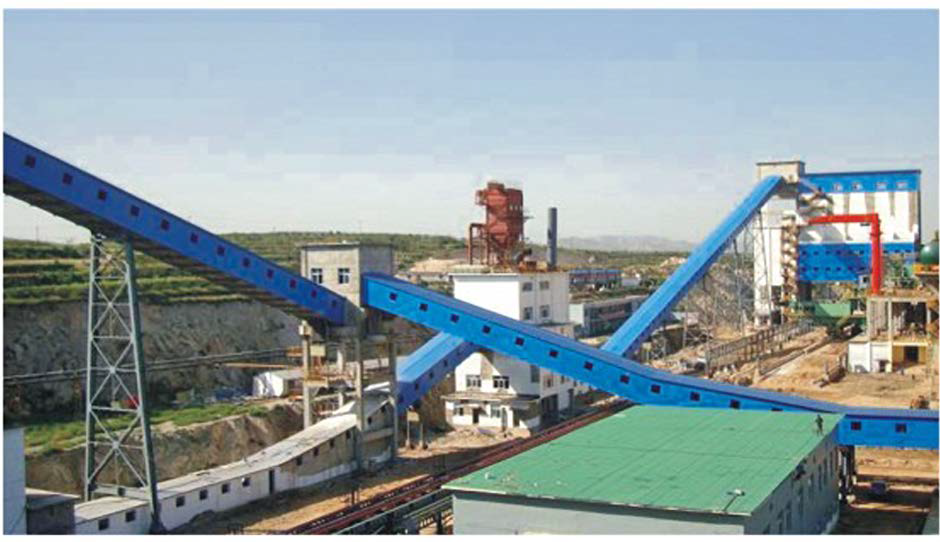
In‑plant belt conveyor
In‑plant belt conveyor is a widely used material conveying equipment in the plant, which enables efficient transportation of bulk materials between production processes.
Small gravel yards realize the local utilization of crushed stone resources.